Remko Booster Pump Solution for a Remote Mine Site
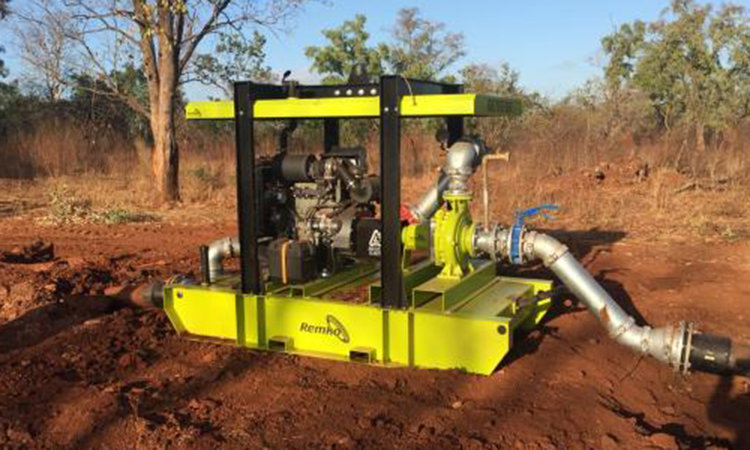
Remko booster pump solution engineered to double water flow over a 16 km pipeline for a remote mining operation.
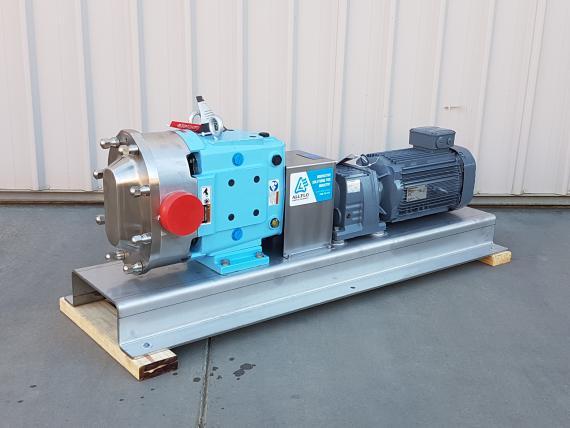
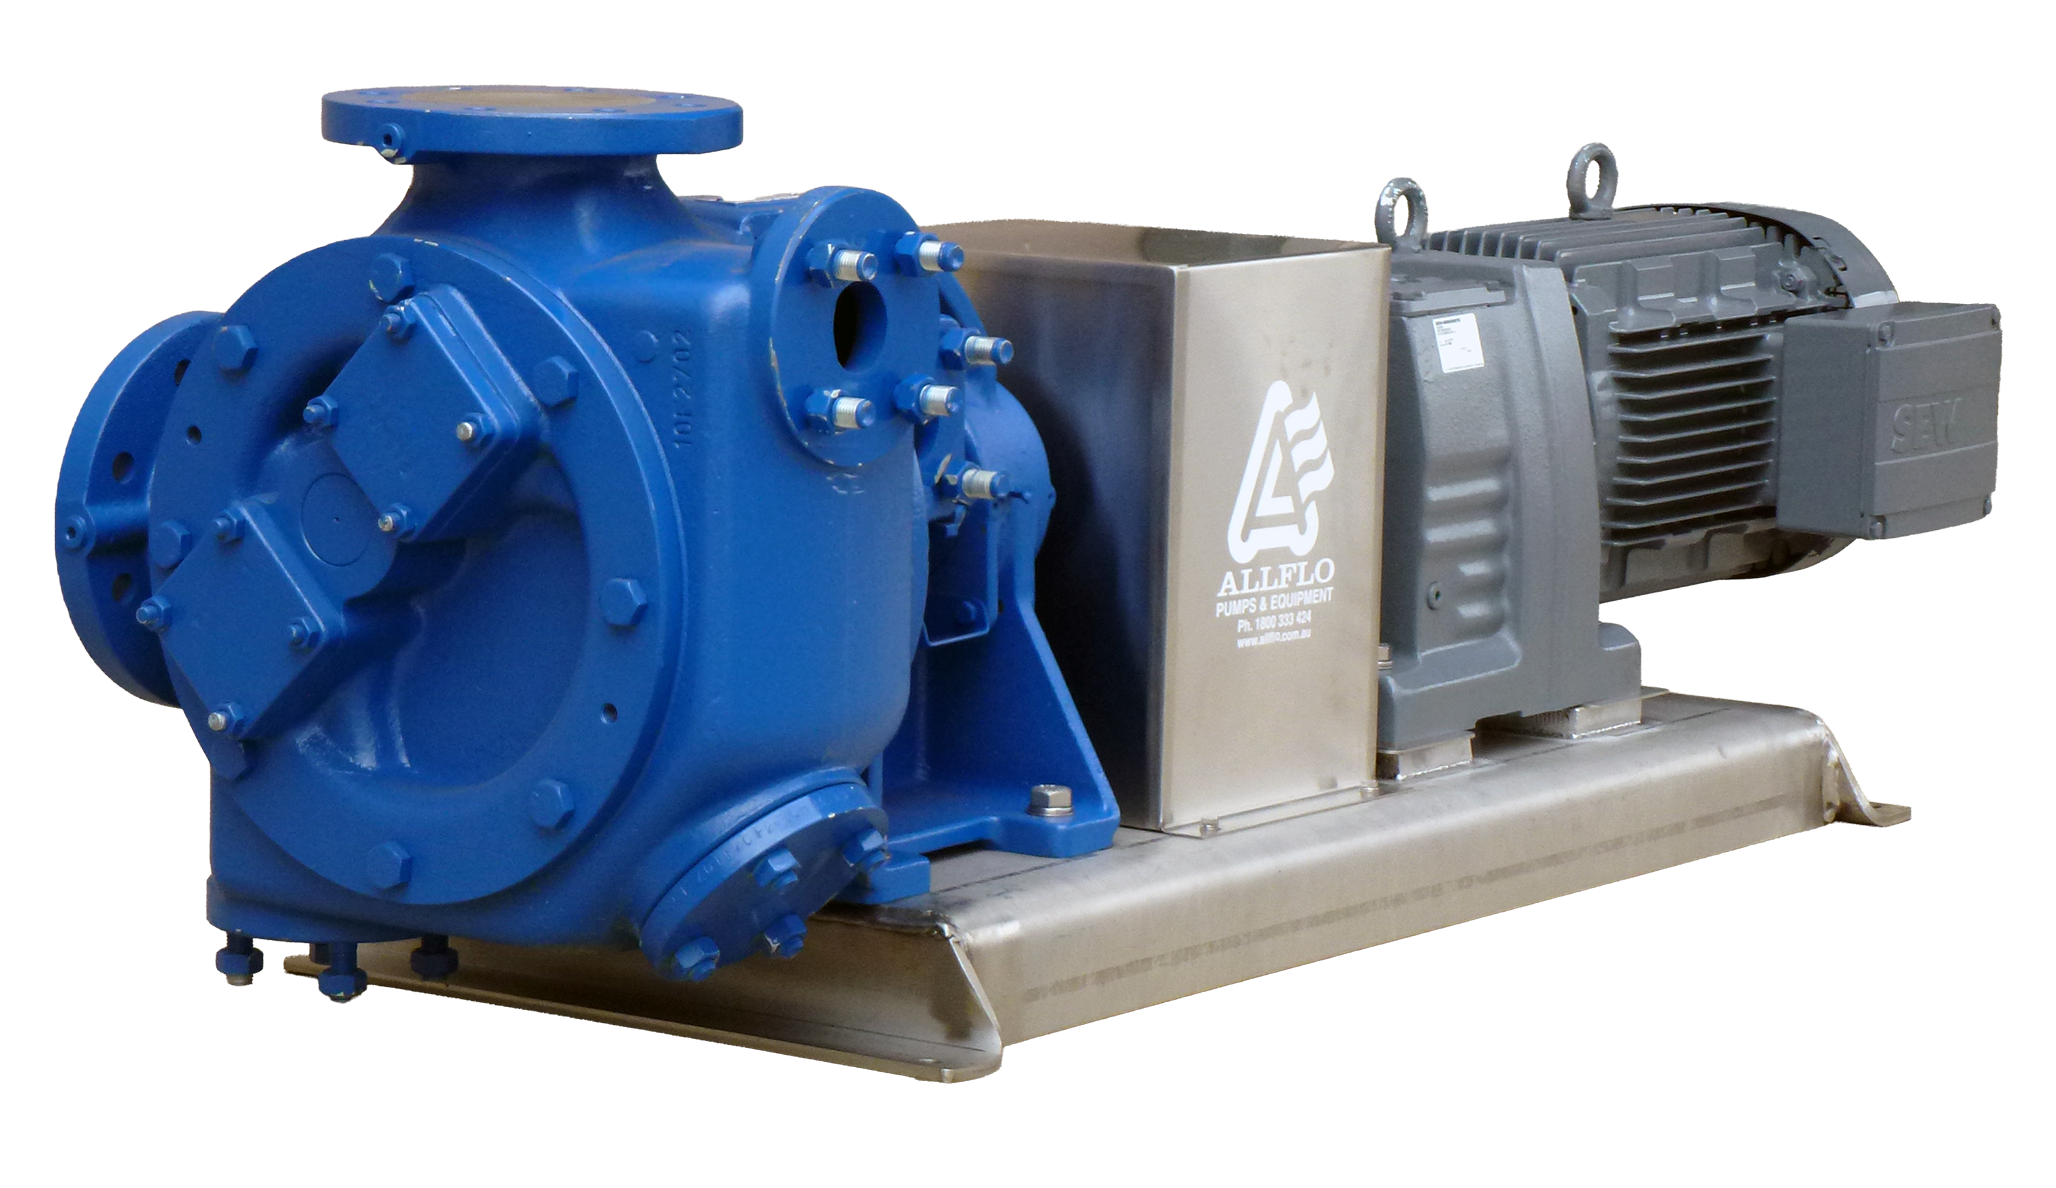
The pumps were mounted on a custom stainless steel base plate, engineered to provide maximum rigidity for continuous-duty operation.
Each pumpset was supplied complete with:
The configuration ensured stable operation under continuous load while supporting hygiene and maintenance requirements typical of chocolate processing applications.
The client was highly satisfied with both the supplied solution and the level of technical support provided by Allflo. Confidence was also expressed in Allflo’s ongoing after-sales support, reinforcing the long-term value of the partnership.
Allflo has extensive experience delivering pump solutions across a wide range of food and viscous liquid applications.
These include:
Allflo specialises in engineered pumping solutions for food and liquid transfer applications, where performance, cleanliness and reliability are essential.
Remko booster pump solution engineered to double water flow over a 16 km pipeline for a remote mining operation.
Custom Waukesha lobe pump solution for a critical food processing application, engineered with a sanitary stainless steel base for easy cleaning.
Diesel auto-prime pump solution for a quarry sand wash plant, delivering high flow, low noise, and reliable performance in demanding site conditions.