1 min read

Lobe Pump for a Critical Food Processing Application

Lobe Pump for a Critical Food Processing Application
Allflo Pumps & Equipment was engaged to supply a lobe pump solution for a critical process application within a food processing plant, where hygiene, reliability and cleanability were essential.


The Challenge

The application required a pumping system that met strict food processing standards while allowing easy access for cleaning and sanitation. Eliminating potential hygiene risks, such as dead spots and inaccessible surfaces, was a key design requirement.


The Allflo Solution

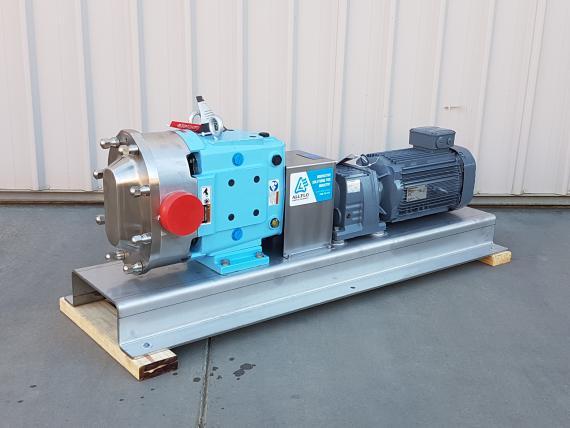
Allflo supplied a Waukesha lobe pump, integrated into a custom-engineered pumpset fabricated in-house by Allflo’s precision engineering team.

Key design features included:

  • A sanitary stainless steel base with open ends, allowing full access for wash-down and cleaning
  • A foot-mounted geared motor, installed on milled stainless steel blocks
  • Seamless welded construction to eliminate crevices and minimise the risk of bacterial growth
  • A layout designed to reduce hygiene risk while maintaining reliable process performance

The complete pumpset was assembled and finished in-house to ensure compliance with food processing requirements.


Outcome

The finished pumpset delivered a hygienic, fit-for-purpose solution suitable for a critical food processing environment, providing the client with confidence in both performance and cleanability.

This project demonstrates Allflo’s capability to deliver custom-engineered pumping solutions for food and beverage applications, where sanitation and precision design are critical.


If you’re assessing pumping solutions for a food processing application, Allflo can assist with selecting and configuring equipment to suit your process and compliance requirements.


Speak with our team


Decanting High-Viscosity Product for a NSW Start-Up

Decanting High-Viscosity Product for a NSW Start-Up

How Allflo helped a NSW start-up decant high-viscosity shampoo efficiently with a complete pump system and remote commissioning support.
Read More
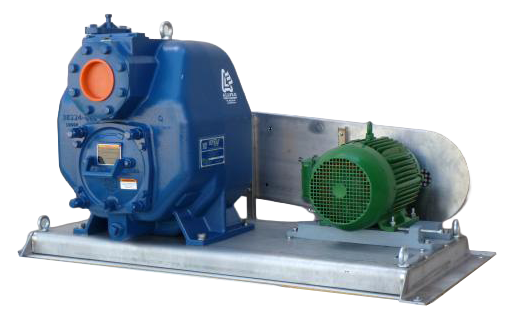
Replacement Gorman-Rupp Pump for Trade Waste Application

Replacement Gorman-Rupp Pump for Trade Waste Application

Like-for-like replacement Gorman-Rupp trade waste pump supplied with upgraded stainless-steel base, delivered on time and within budget.
Read More
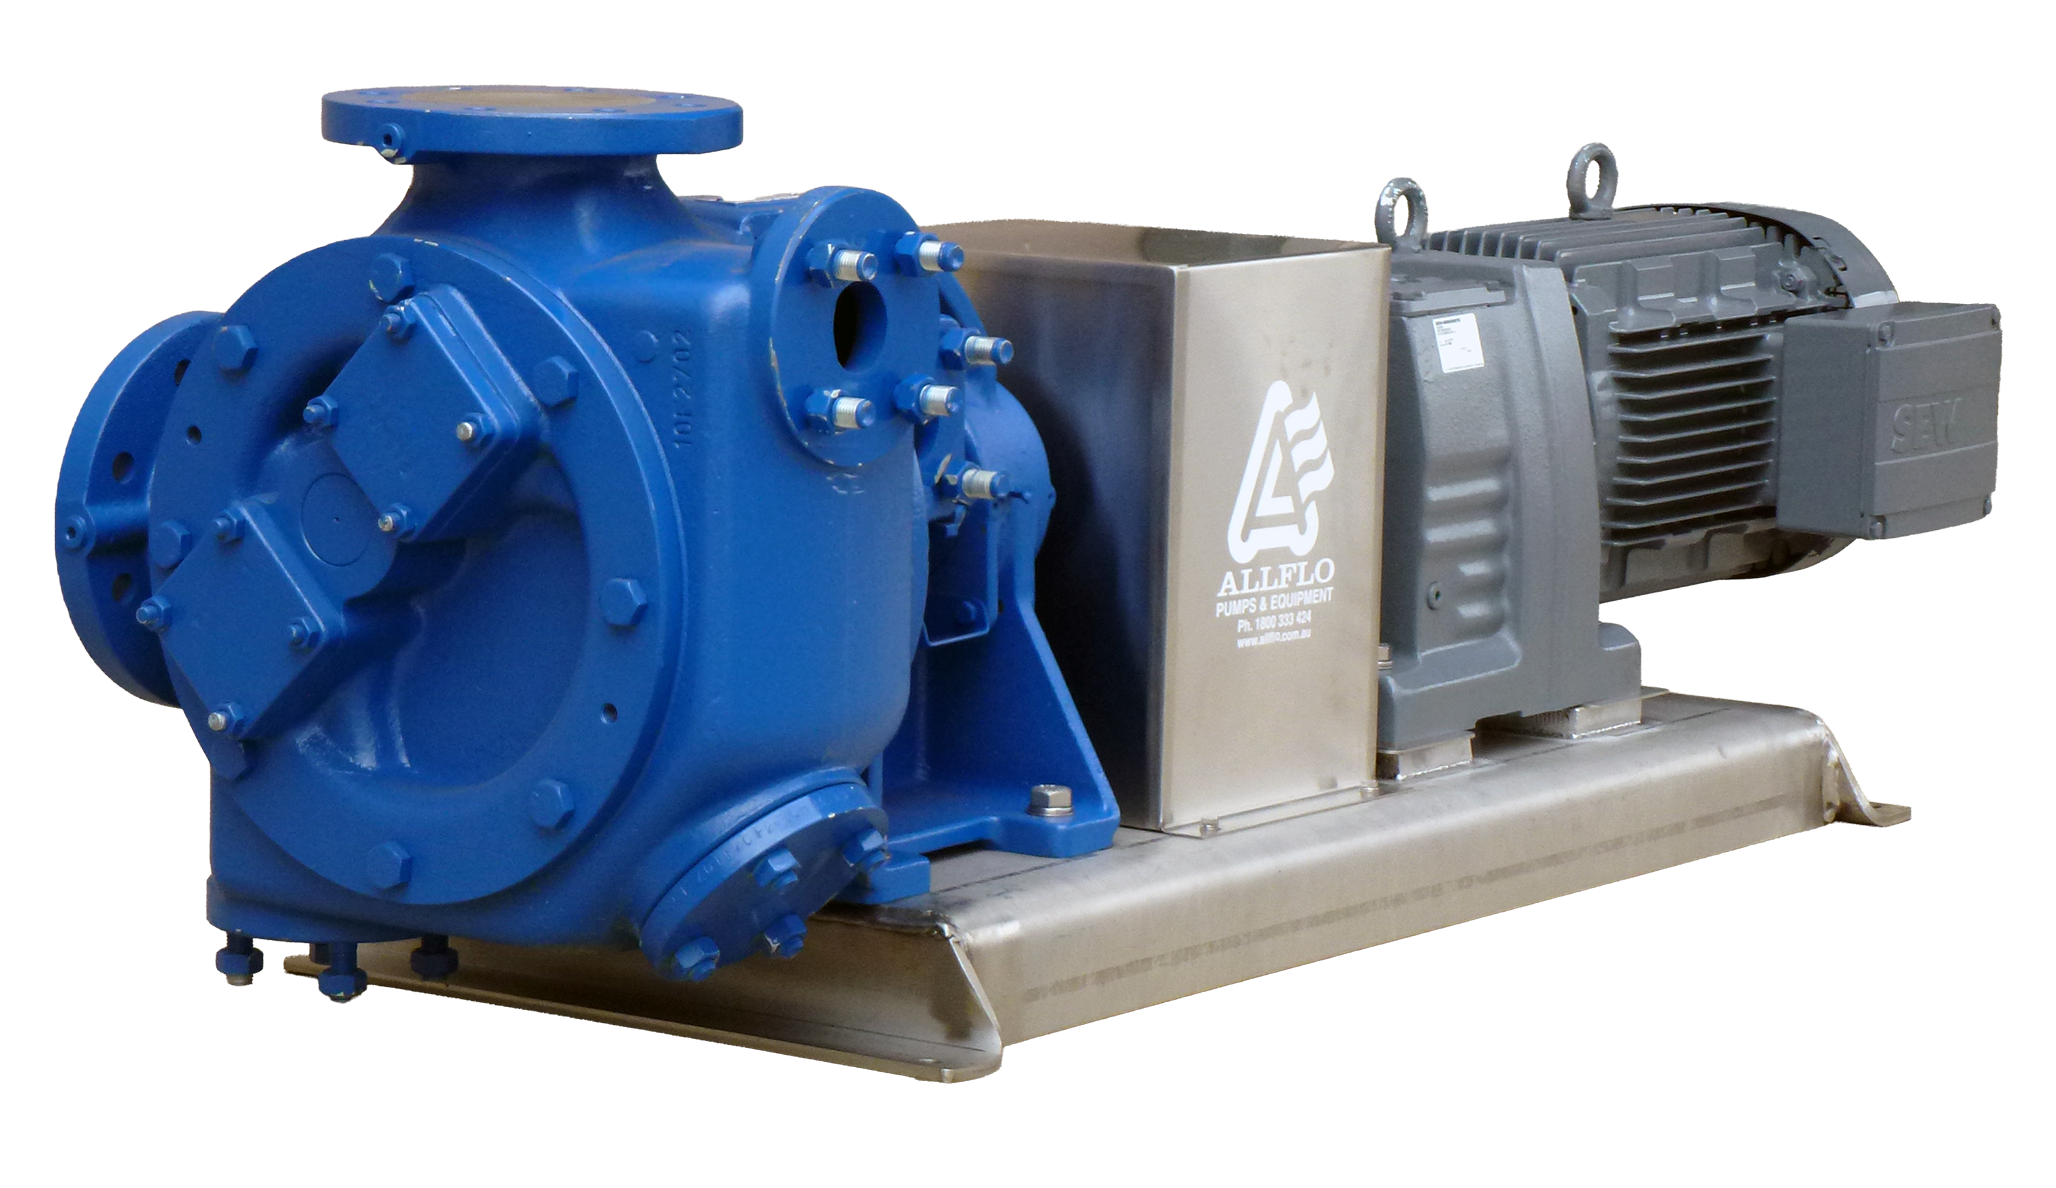
Replacement of Large Chocolate Transfer Pumps

Replacement of Large Chocolate Transfer Pumps

Custom stainless steel chocolate transfer pumps supplied with geared motors for reliable, continuous food processing applications.

Read More