1 min read

Remko Booster Pump Solution for a Remote Mine Site

Remko Booster Pump Solution for a Remote Mine Site
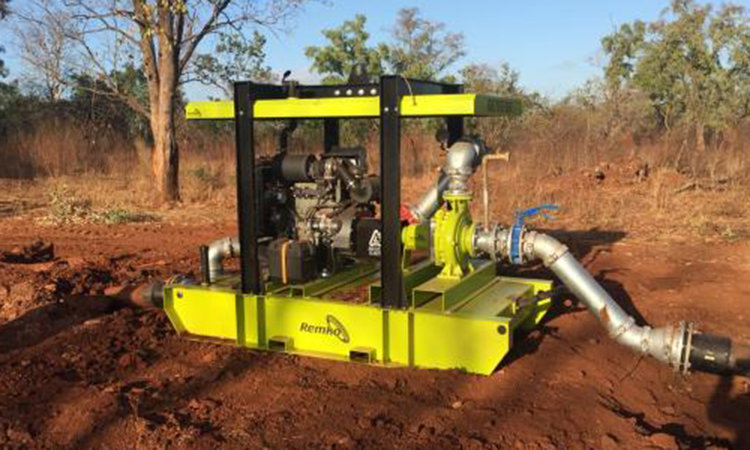
Allflo Pumps & Equipment was engaged to deliver a booster pumping solution to transfer water from a river to a remote mine site, where water supply was critical to plant operation and production continuity.


The Challenge

The mine relied on a 16 km pipeline as its primary water supply. The existing pump installation was unable to deliver sufficient flow, restricting plant performance and threatening production targets.

Key challenges included:

  • Maximising flow over a long pipeline distance
  • Preventing over-pressurisation of existing pipework
  • Maintaining stable and reliable water supply to the site

The Allflo Solution

Allflo’s application engineering team assessed the system using pipeline data and contour mapping to fully understand elevation changes and friction losses.

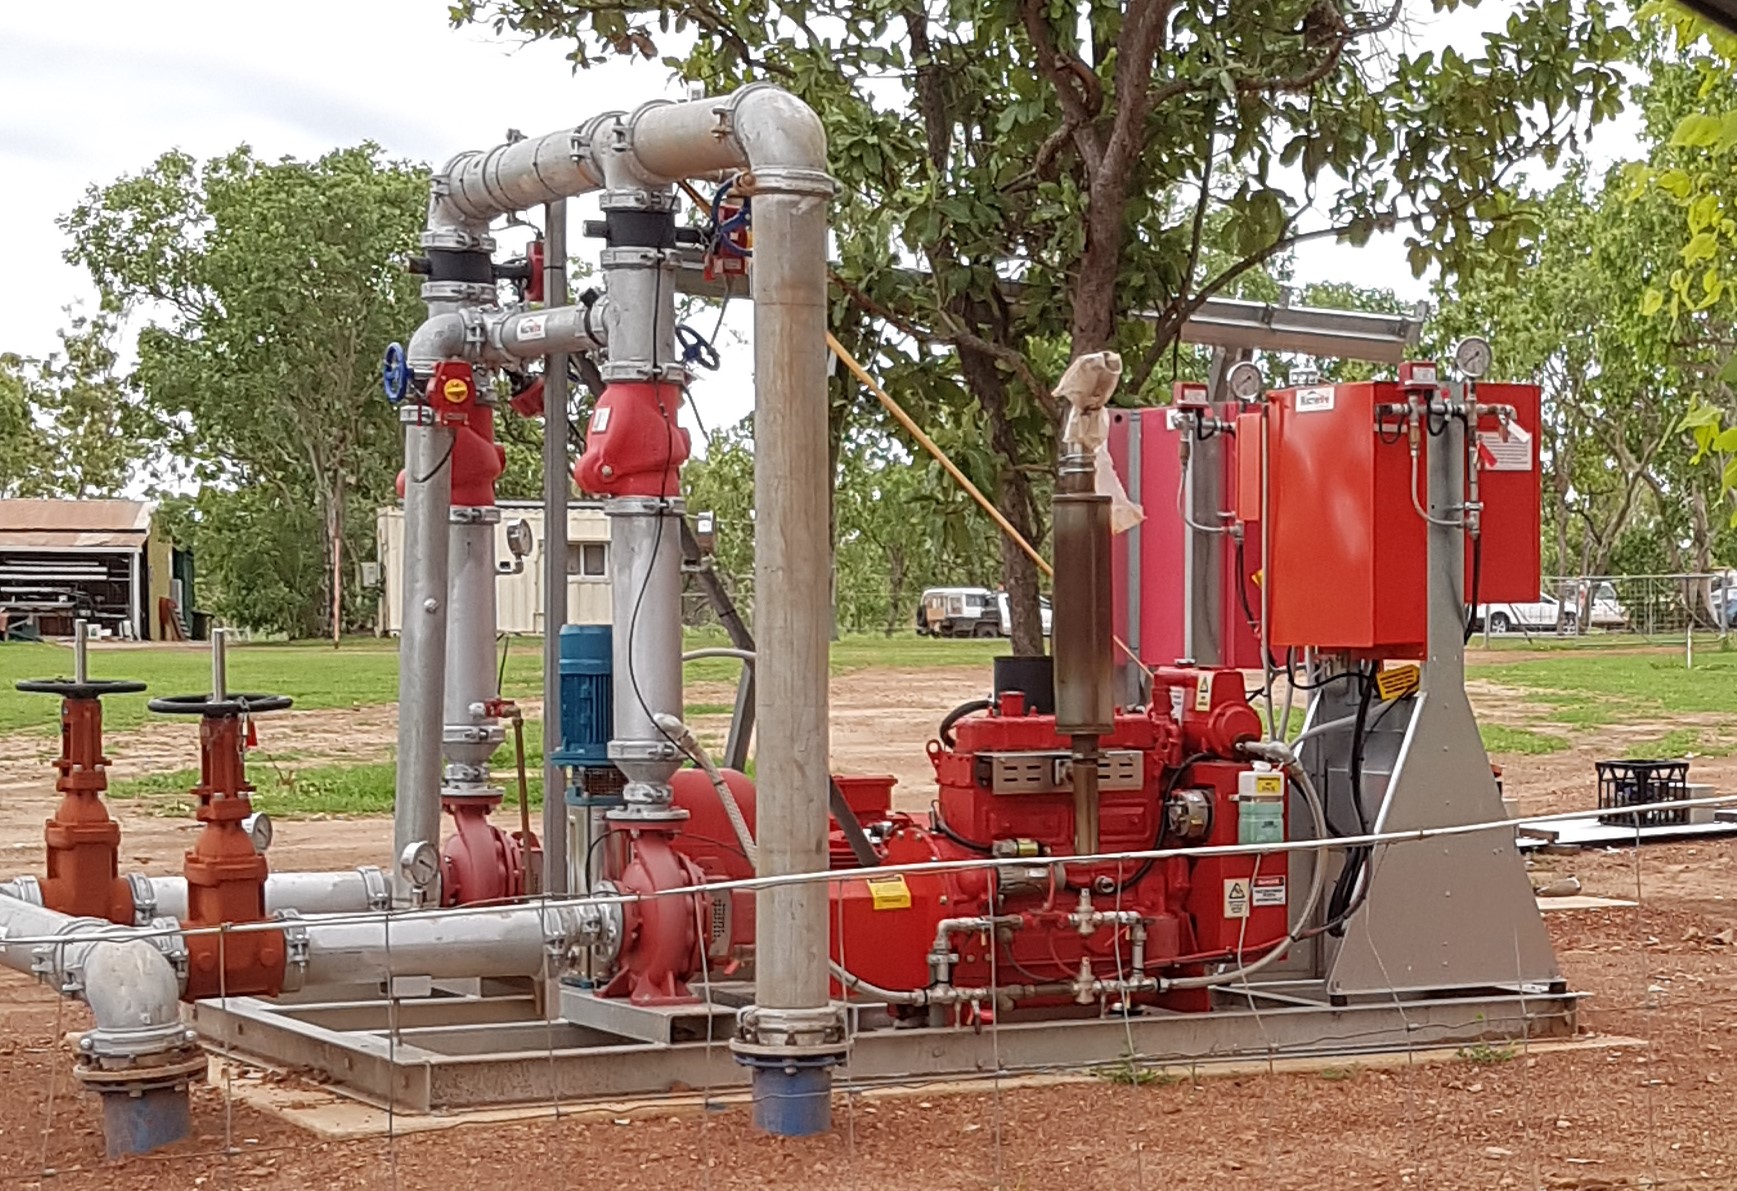
The solution involved supplying a booster pumpset designed to optimise flow while protecting the pipeline.

The selected system:

  • Doubled the available flow to the plant
  • Used automatic pressure control via pressure transducers
  • Incorporated variable speed operation, allowing pump output to increase or decrease based on discharge pressure
  • Prevented over-pressurisation while maximising throughput

A Remko booster pump solution was selected to meet the duty requirements and operate reliably in a remote mining environment.


Outcome

The upgraded booster pumping system restored reliable water supply to the site and enabled the mine to operate at production levels required for ongoing profitability.

This project demonstrates Allflo’s capability to deliver engineered pumping solutions for long-distance water transfer in remote mining applications, where performance, control, and system protection are critical.


Speak with Allflo to discuss booster pumping solutions for mining and remote water transfer applications.


Talk to a Pump Expert

Remote Mine Camp Protected with Engineered Pump Systems

Remote Mine Camp Protected with Engineered Pump Systems

Engineered pumping solution delivered by Allflo for a remote NT mining accommodation village, demonstrating robust design and project delivery...
Read More
Replacement of Large Chocolate Transfer Pumps

Replacement of Large Chocolate Transfer Pumps

Custom stainless steel chocolate transfer pumps supplied with geared motors for reliable, continuous food processing applications.
Read More
Queensland Abattoir Chooses Remko for Trade Waste Upgrade

Queensland Abattoir Chooses Remko for Trade Waste Upgrade

Heavy-duty Remko trash pumps selected for a Queensland abattoir trade waste upgrade, handling high solids and increased production demands.

Read More