Lobe Pump for a Critical Food Processing Application
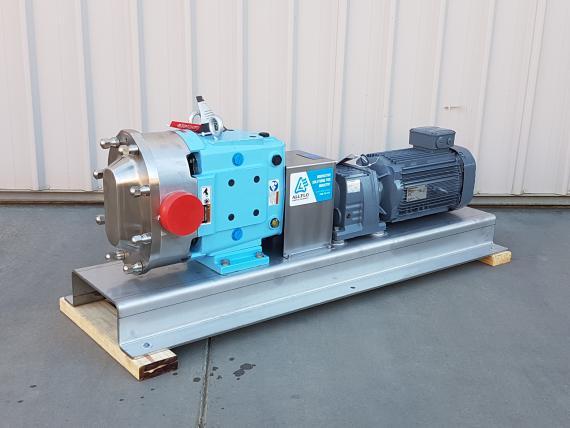
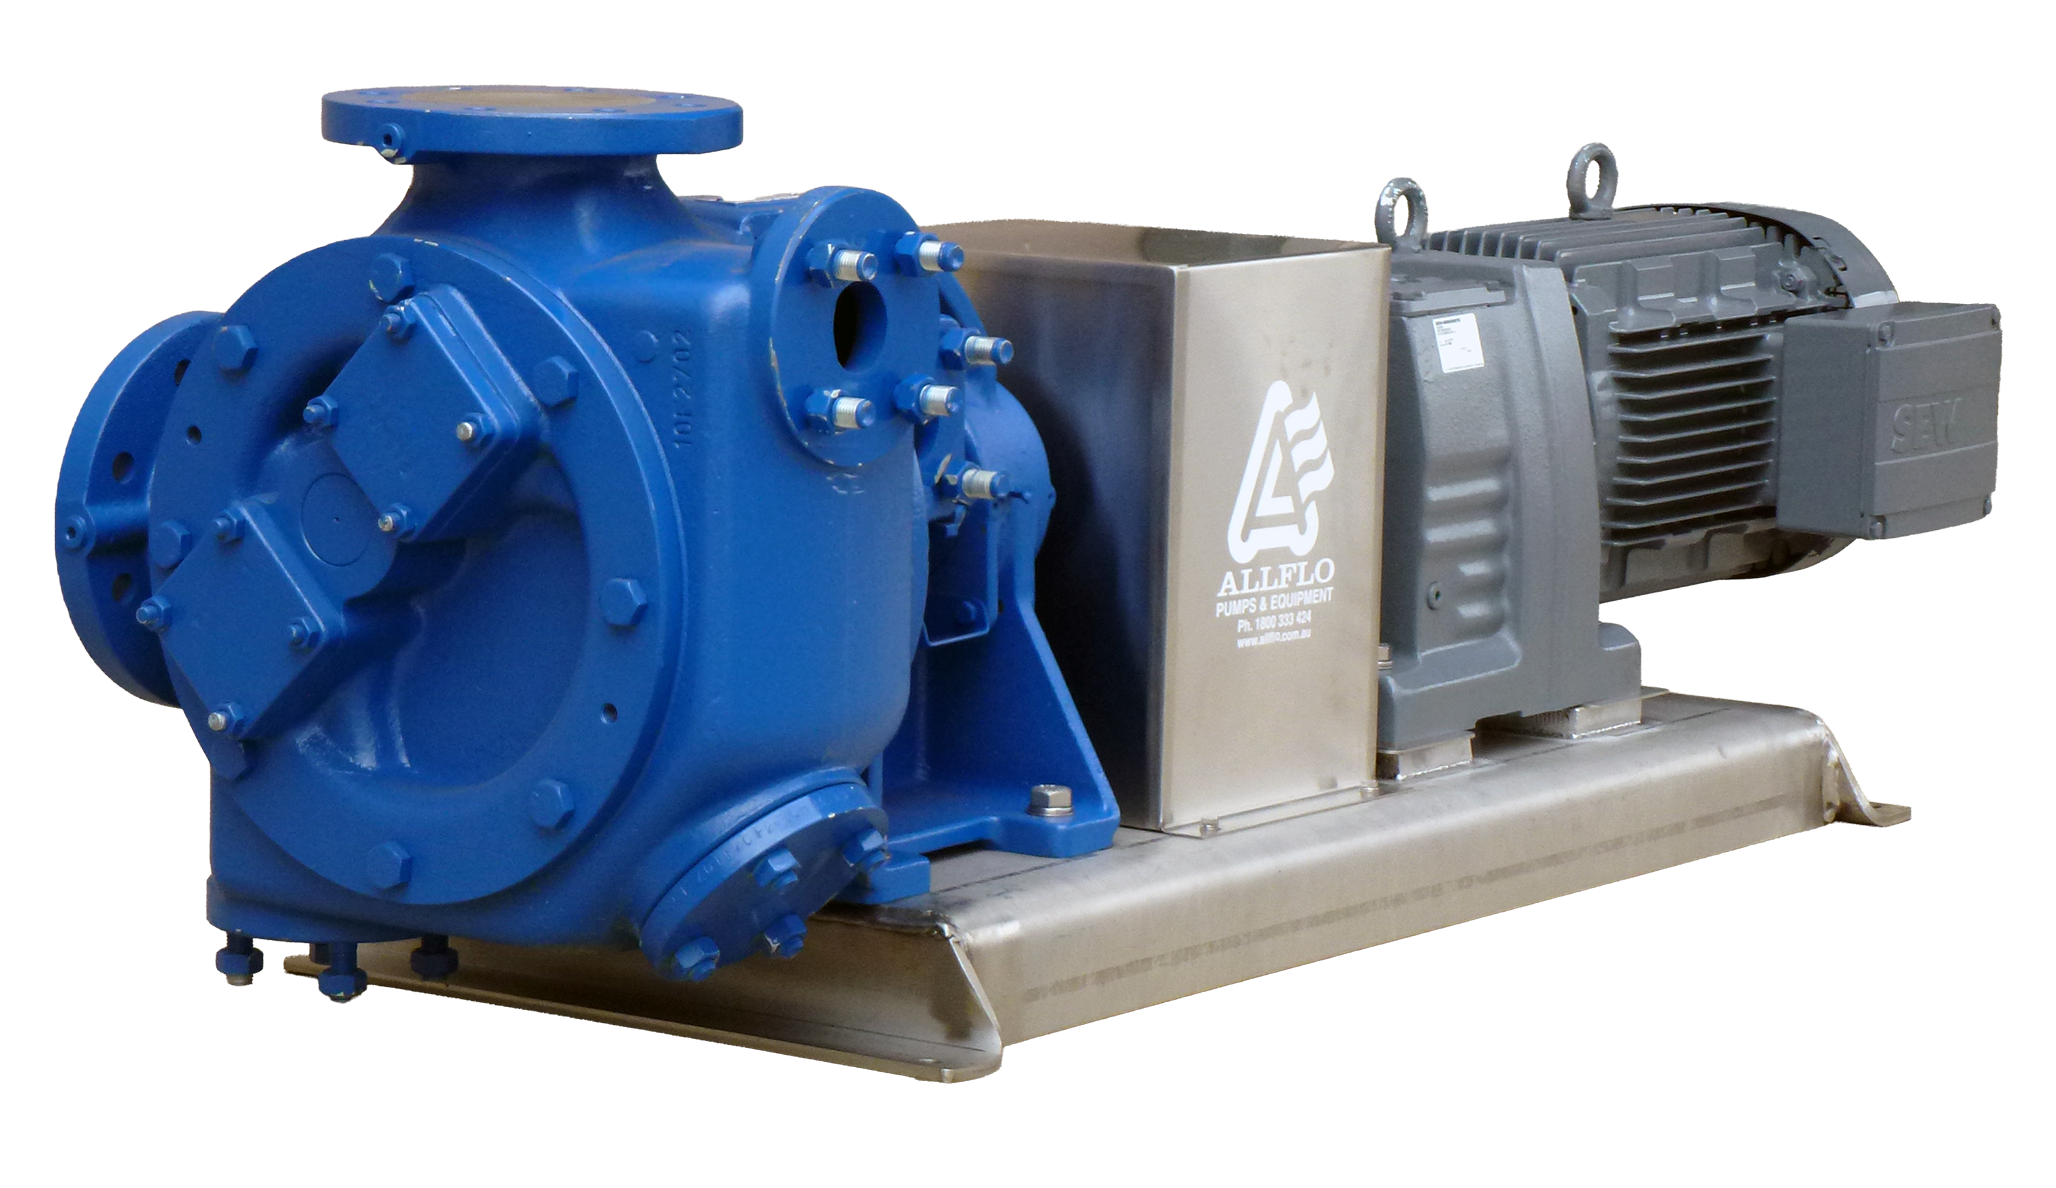
Custom Waukesha lobe pump solution for a critical food processing application, engineered with a sanitary stainless steel base for easy cleaning.
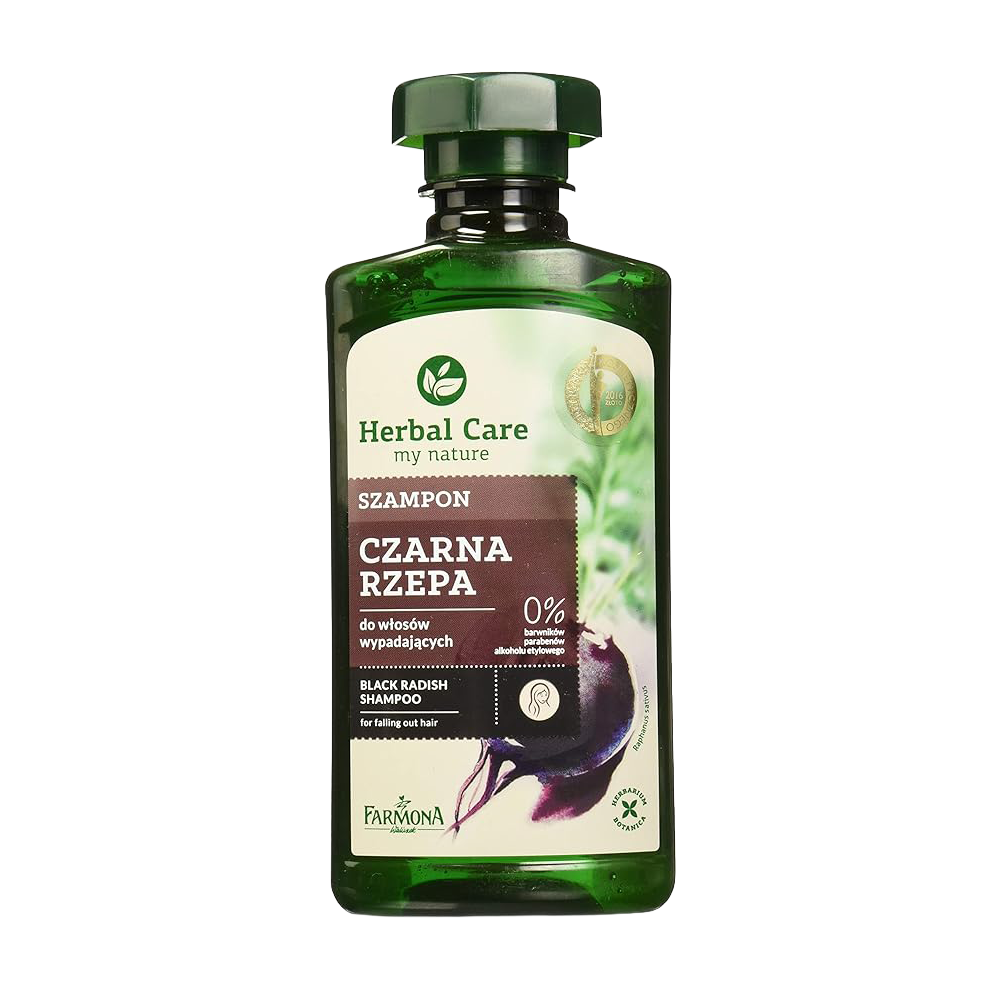
A new start-up in eastern New South Wales required a reliable way to transfer a high-viscosity shampoo from bulk drums into smaller retail bottles. With limited experience in pumping equipment, the client needed a complete, easy-to-operate solution that would support efficient production from day one.
The system needed to handle thick product consistently, minimise mess and waste, and be simple enough for a small team to operate with confidence.
After finding Allflo online and speaking with our team, the client engaged Allflo to supply a fully integrated decanting system, including:
Recognising the client’s limited technical experience, Allflo provided remote commissioning support, using video calls and simple installation sketches to guide setup and operation. This ensured the system was installed correctly and operating efficiently without the need for on-site assistance.
The system was commissioned successfully, allowing the client to transfer and bottle product reliably and efficiently, with full confidence in daily operation. The production line was brought online quickly, enabling the business to supply wholesalers and retailers without disruption.
With a clear understanding of the equipment and ongoing support available from Allflo, the client was able to take ownership of the process and focus on growing their business.
Custom Waukesha lobe pump solution for a critical food processing application, engineered with a sanitary stainless steel base for easy cleaning.
Custom stainless steel chocolate transfer pumps supplied with geared motors for reliable, continuous food processing applications.
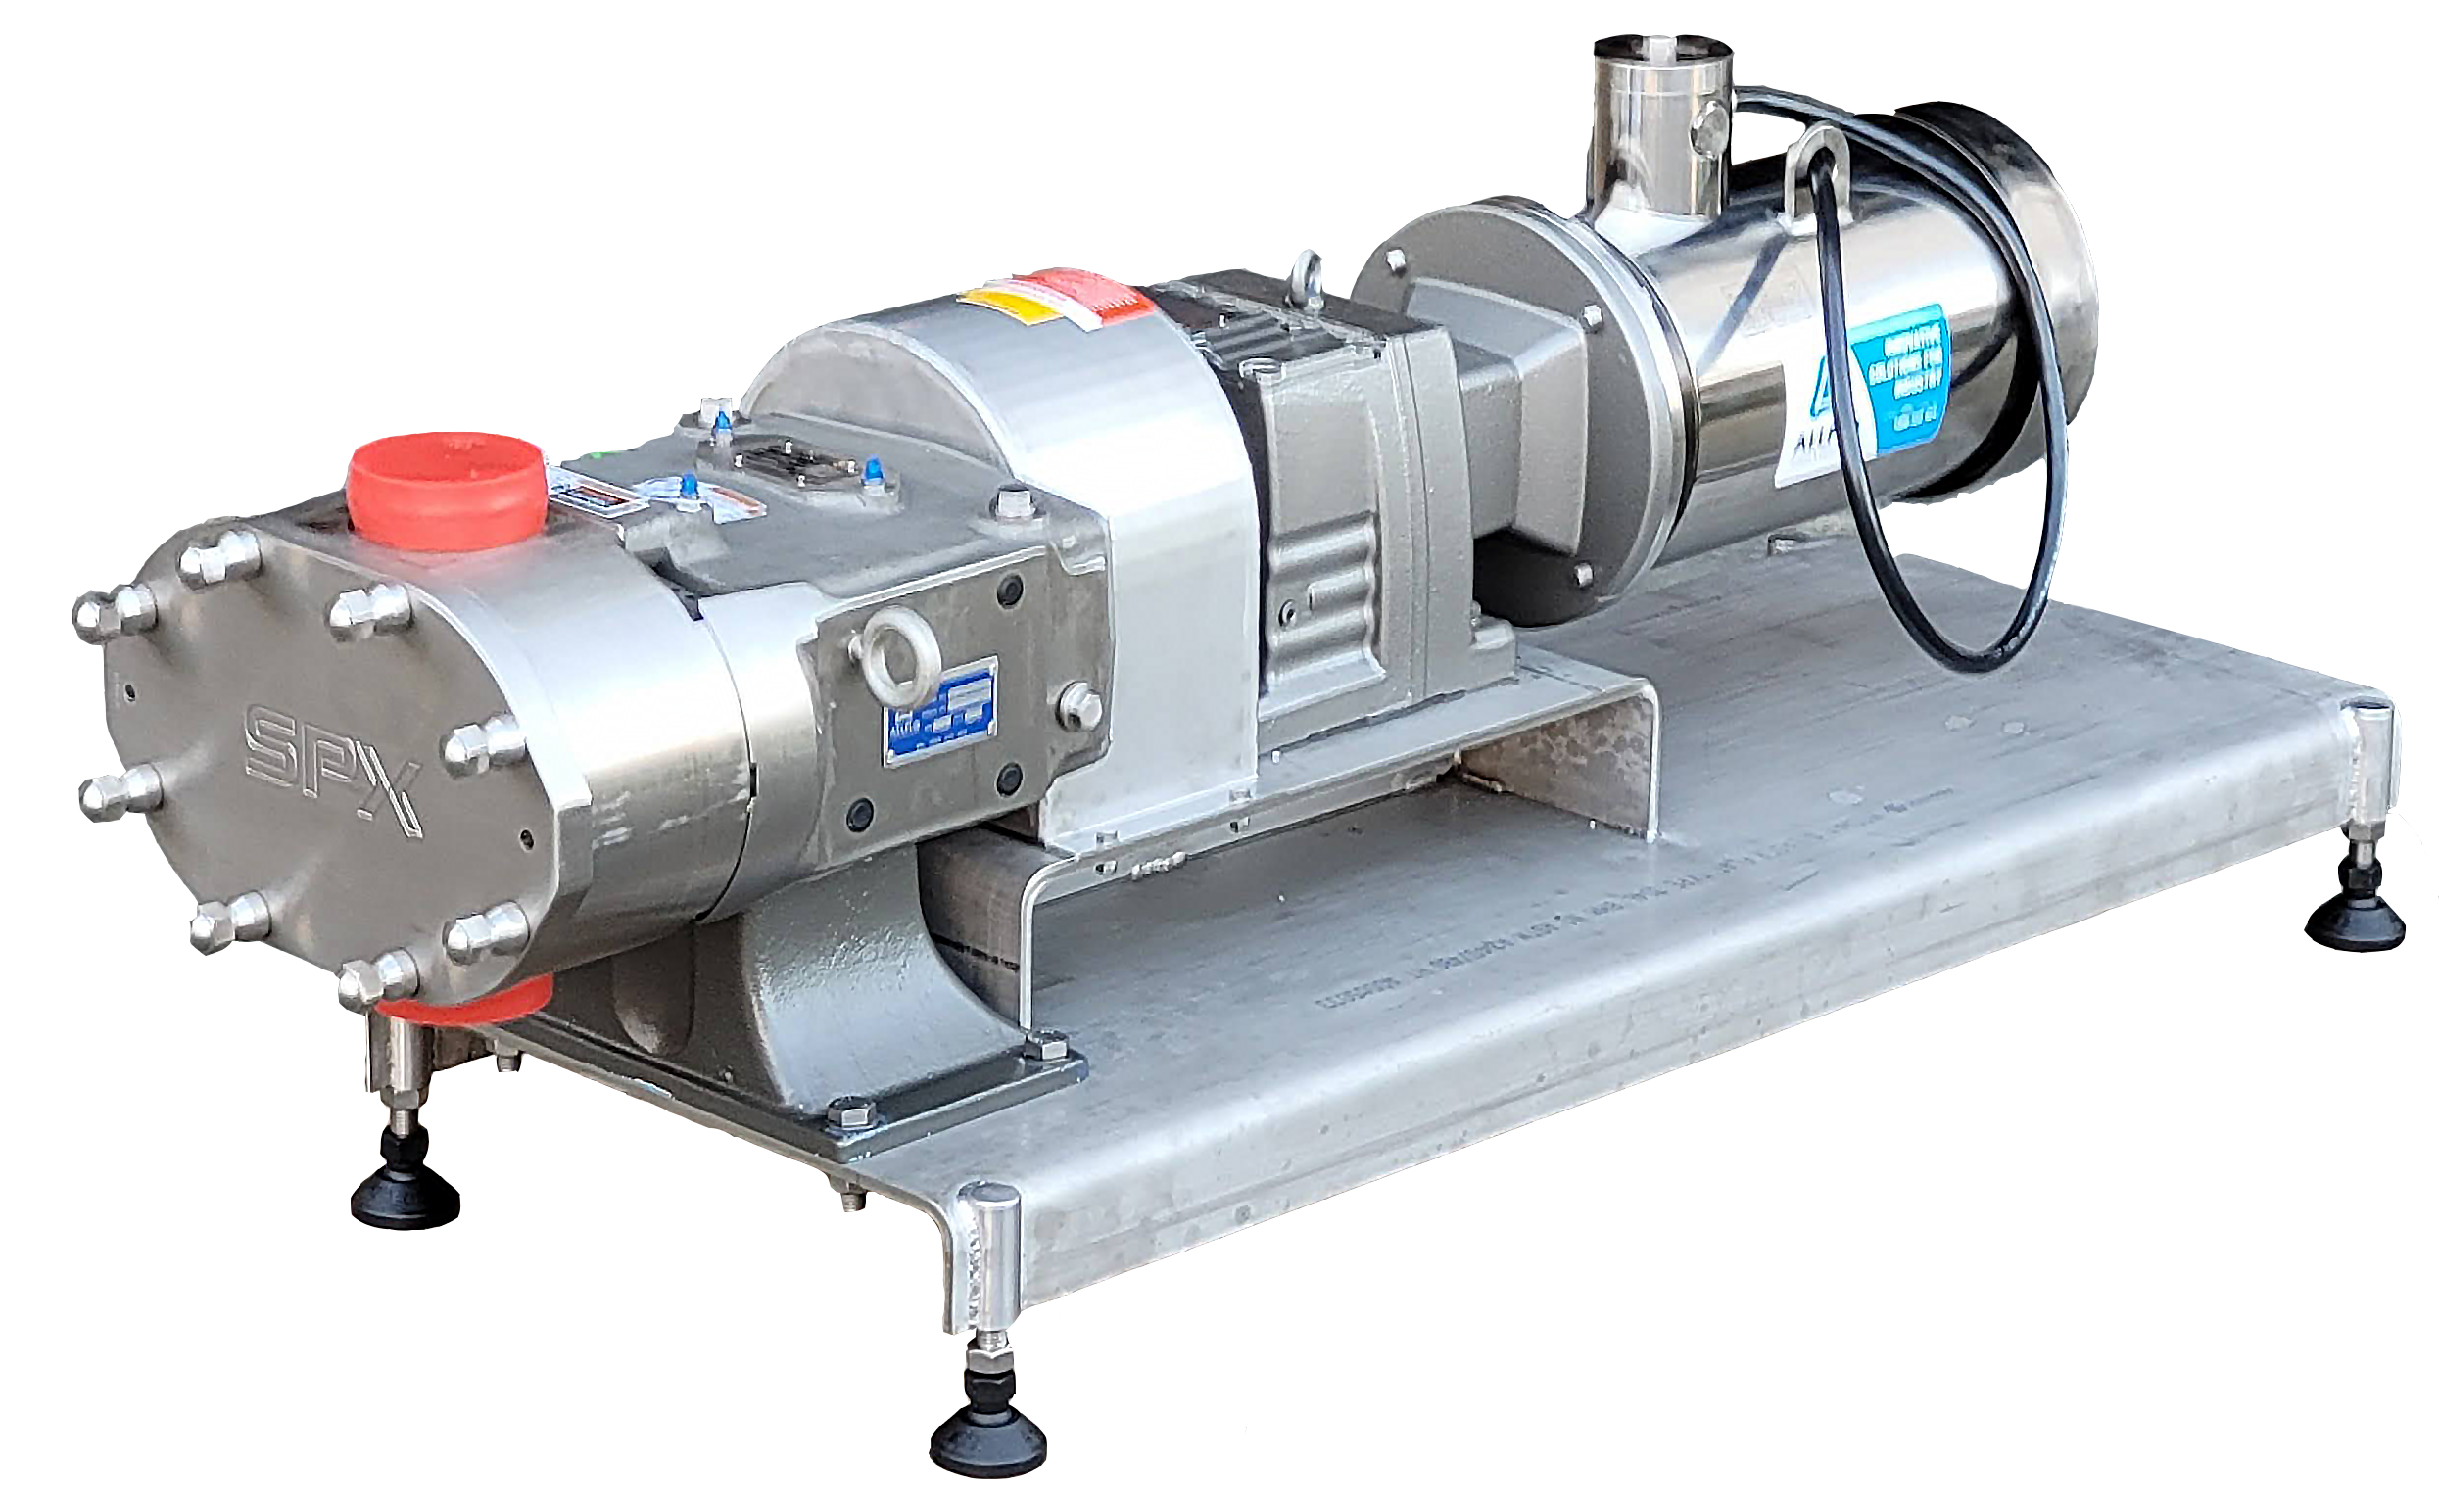
Custom pump base and Waukesha U3 pump solution designed to improve hygiene, maintenance safety, and efficiency in a high-volume dairy plant.