1 min read

Acid Trade Waste Pump Solution

Acid Trade Waste Pump Solution
Managing acidic trade waste requires reliable equipment, appropriate materials and effective containment.

Allflo Pumps was engaged by a chemical processing facility to deliver a safe and robust solution for transferring diluted nitric acid and sulphuric acid.

The Challenge

The system needed to pump acidic waste into a pipeline shared by multiple pumps discharging into a common header, creating risks around corrosion, pressure variation, and potential leakage. Strict safety and containment standards also had to be met.

The Allflo Solution

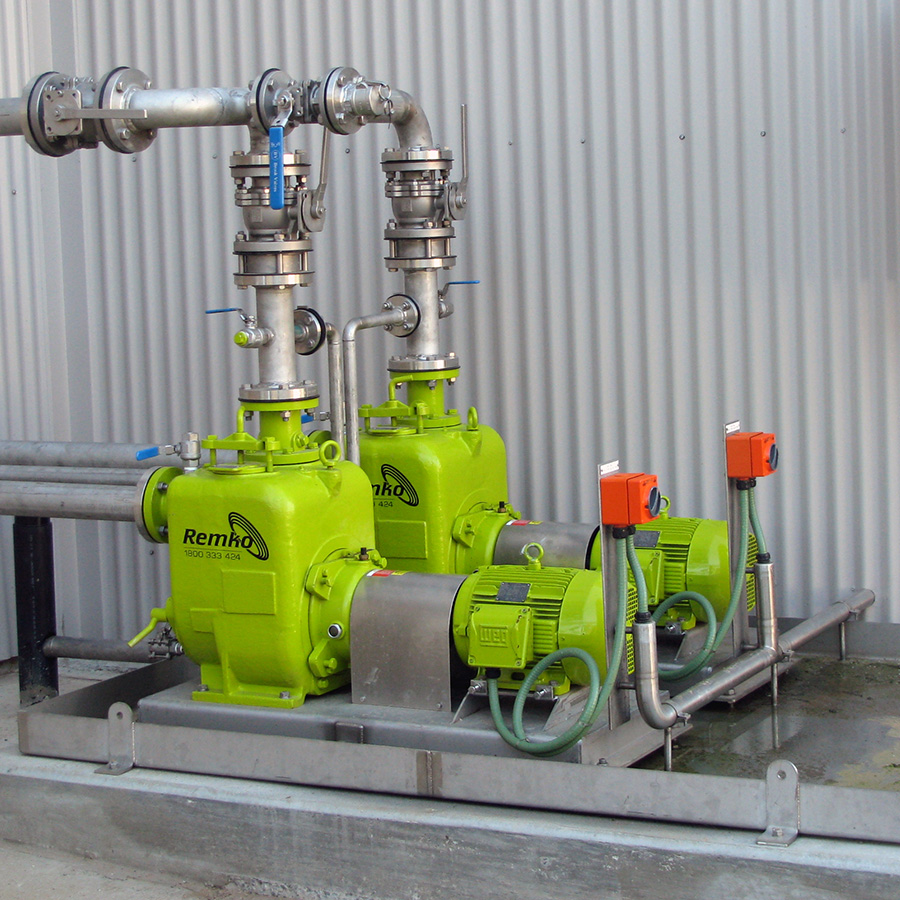
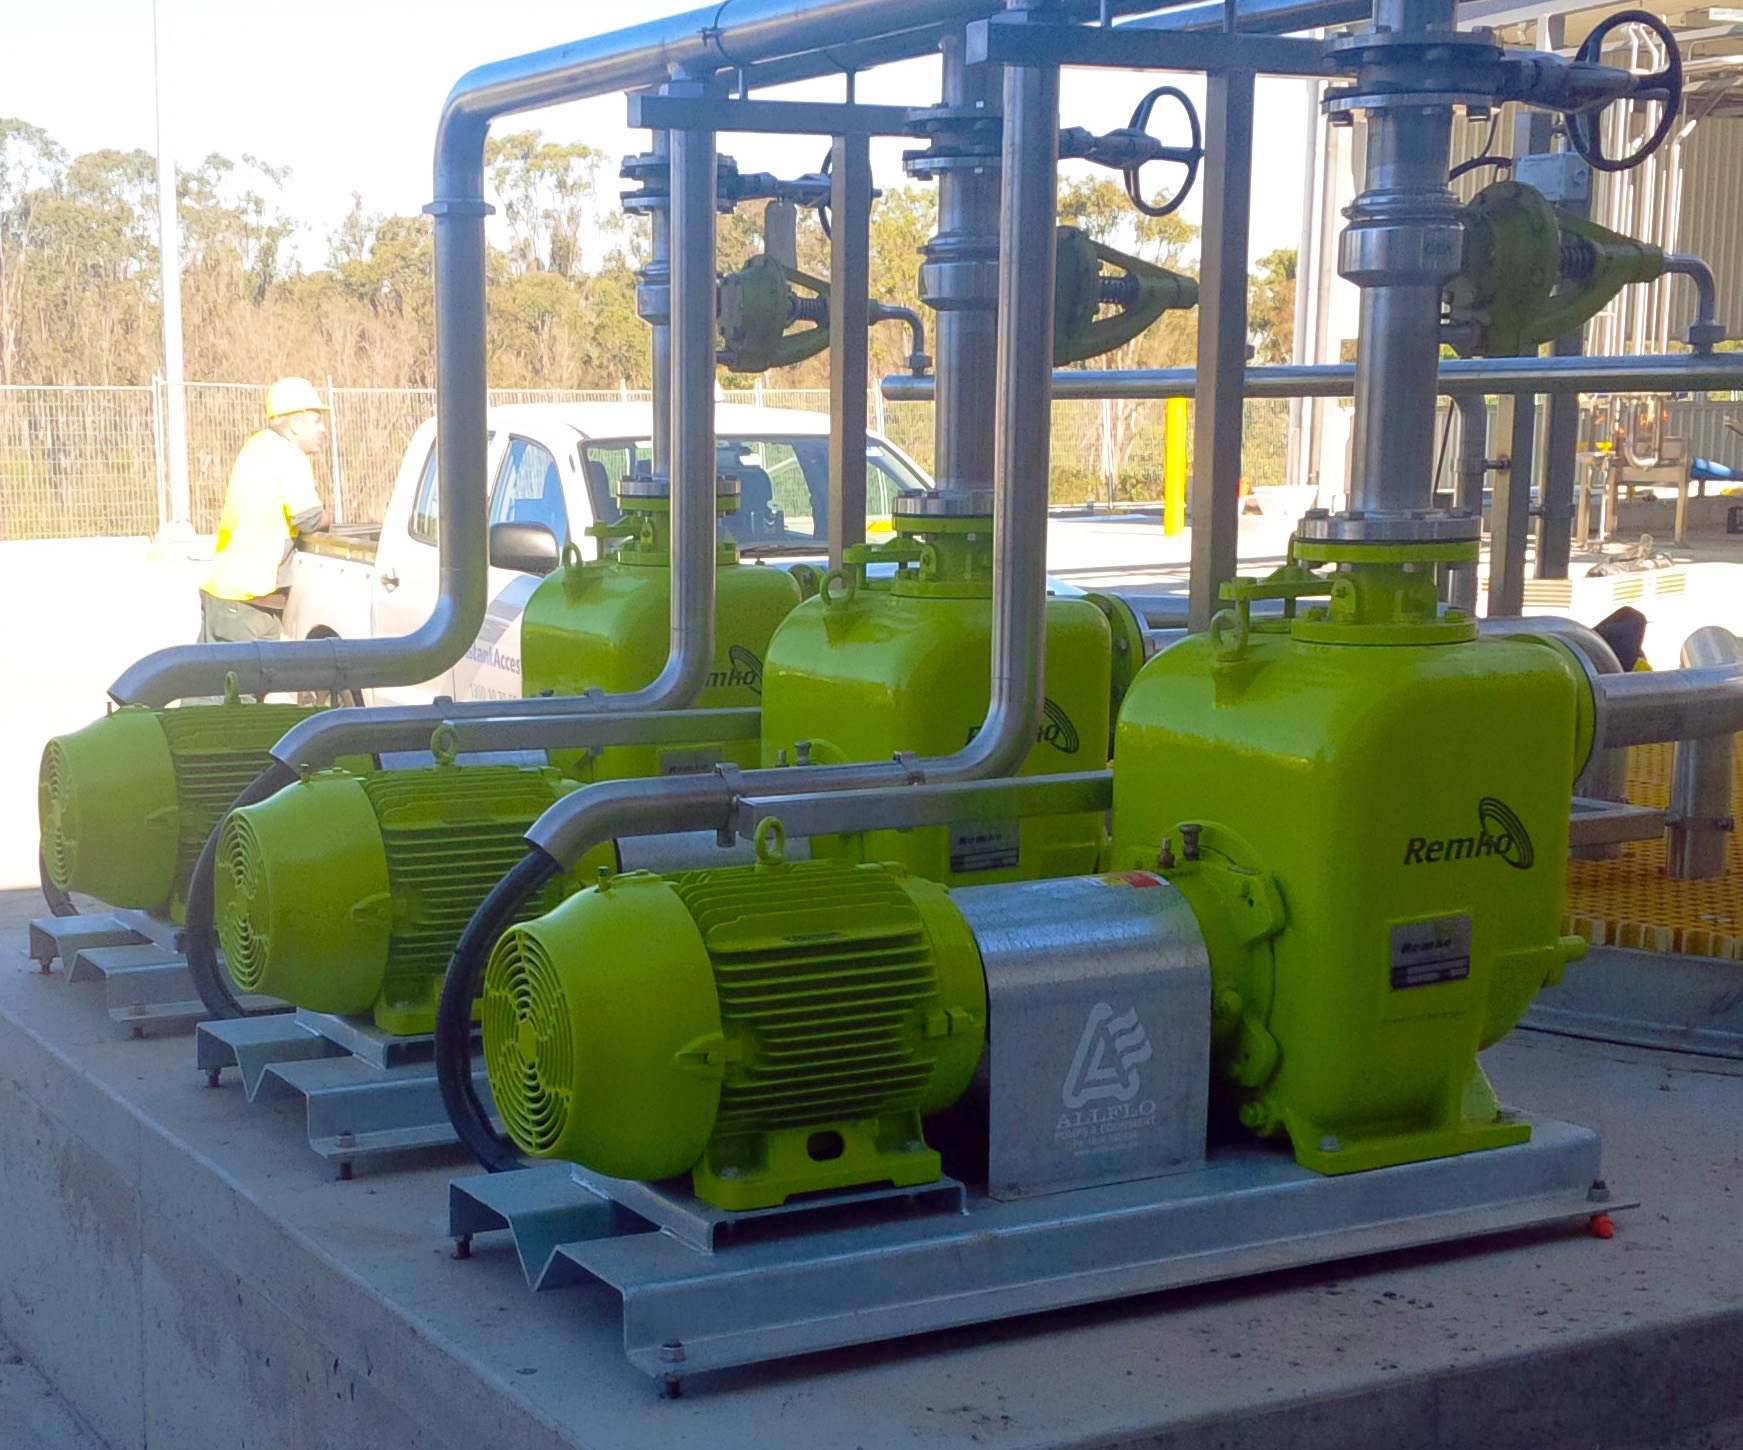
Allflo designed and manufactured a custom-engineered acid handling pumpset, tailored to the application.

The solution included:

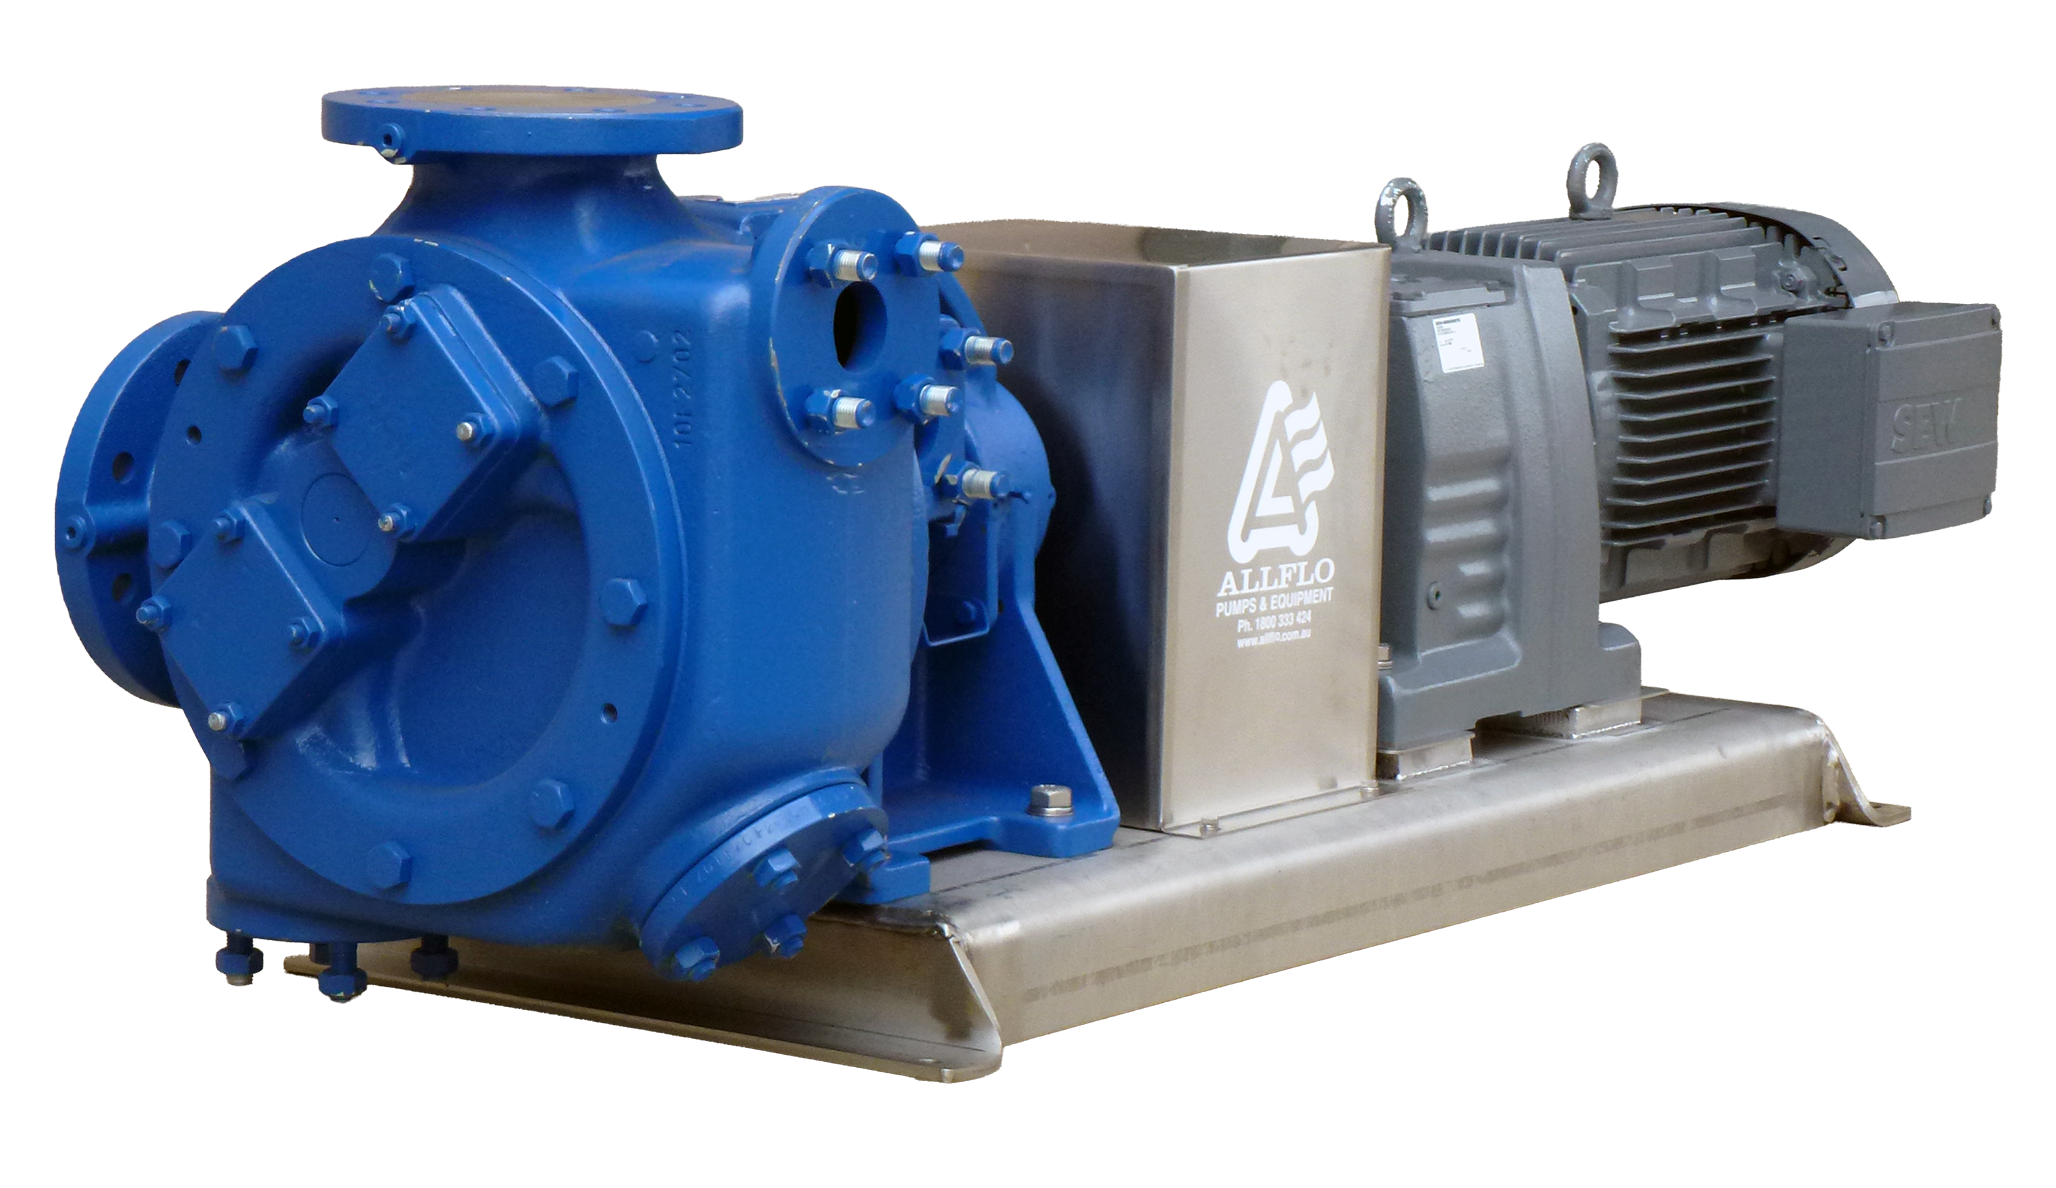
  • Remko 316 stainless steel self-priming pumps

  • Full 316 stainless steel construction for corrosion resistance

  • A heavy-duty stainless steel base

  • Installation within a stainless steel bunded area for spill containment

  • Custom stainless steel pipework and valves, fabricated and installed on site

Performance

The pumpset was commissioned successfully and is operating as specified:

  • Flow rate: 18 litres per second

  • Discharge pressure: 220 kPa

Outcome

This project demonstrates Allflo’s capability to deliver engineered pumping solutions for corrosive and high-risk trade waste applications, where safety, reliability, and material selection are critical.

If you’re managing acidic trade waste or chemical transfer, Allflo can design a solution to suit your site and compliance requirements.

Speak with our Industrial pump specialists


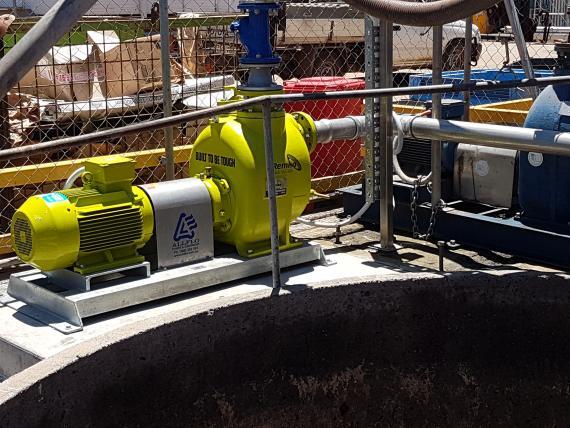
Remko Trade Waste Pumps for Dairy Manufacturing Facilities

Remko Trade Waste Pumps for Dairy Manufacturing Facilities

Engineered Remko trade waste pump systems supplied for Australian dairy manufacturing, designed for solids handling and long-term reliability.
Read More
Replacement of Large Chocolate Transfer Pumps

Replacement of Large Chocolate Transfer Pumps

Custom stainless steel chocolate transfer pumps supplied with geared motors for reliable, continuous food processing applications.
Read More
Queensland Abattoir Chooses Remko for Trade Waste Upgrade

Queensland Abattoir Chooses Remko for Trade Waste Upgrade

Heavy-duty Remko trash pumps selected for a Queensland abattoir trade waste upgrade, handling high solids and increased production demands.

Read More