Custom Pump Base Design for Global Leader in the Dairy Industry
Custom pump base and Waukesha U3 pump solution designed to improve hygiene, maintenance safety, and efficiency in a high-volume dairy plant.
1 min read
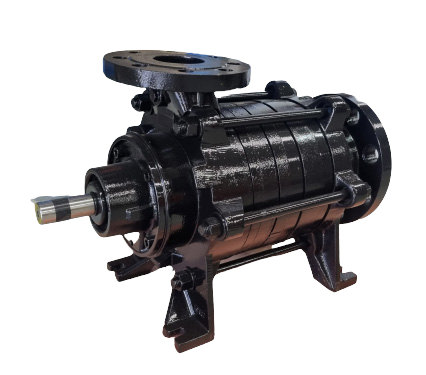

This pump upgrade demonstrates how targeted engineering improvements can significantly improve reliability and extend service life in demanding industrial environments.
In this application, the pump was operating under sustained high pressure and temperature conditions, leading to repeated seal failures and unplanned downtime. Rather than replacing the pump entirely, Allflo assessed the failure points and implemented targeted engineering upgrades — including improved sealing arrangements and materials better suited to the operating conditions.
The result was a significantly more robust pump assembly, reduced maintenance intervention and a substantial extension of service life.
These improvements quadrupled the pump's life.
This kind of targeted upgrade allows existing assets to perform reliably in harsh conditions, without the cost and disruption of full replacement.
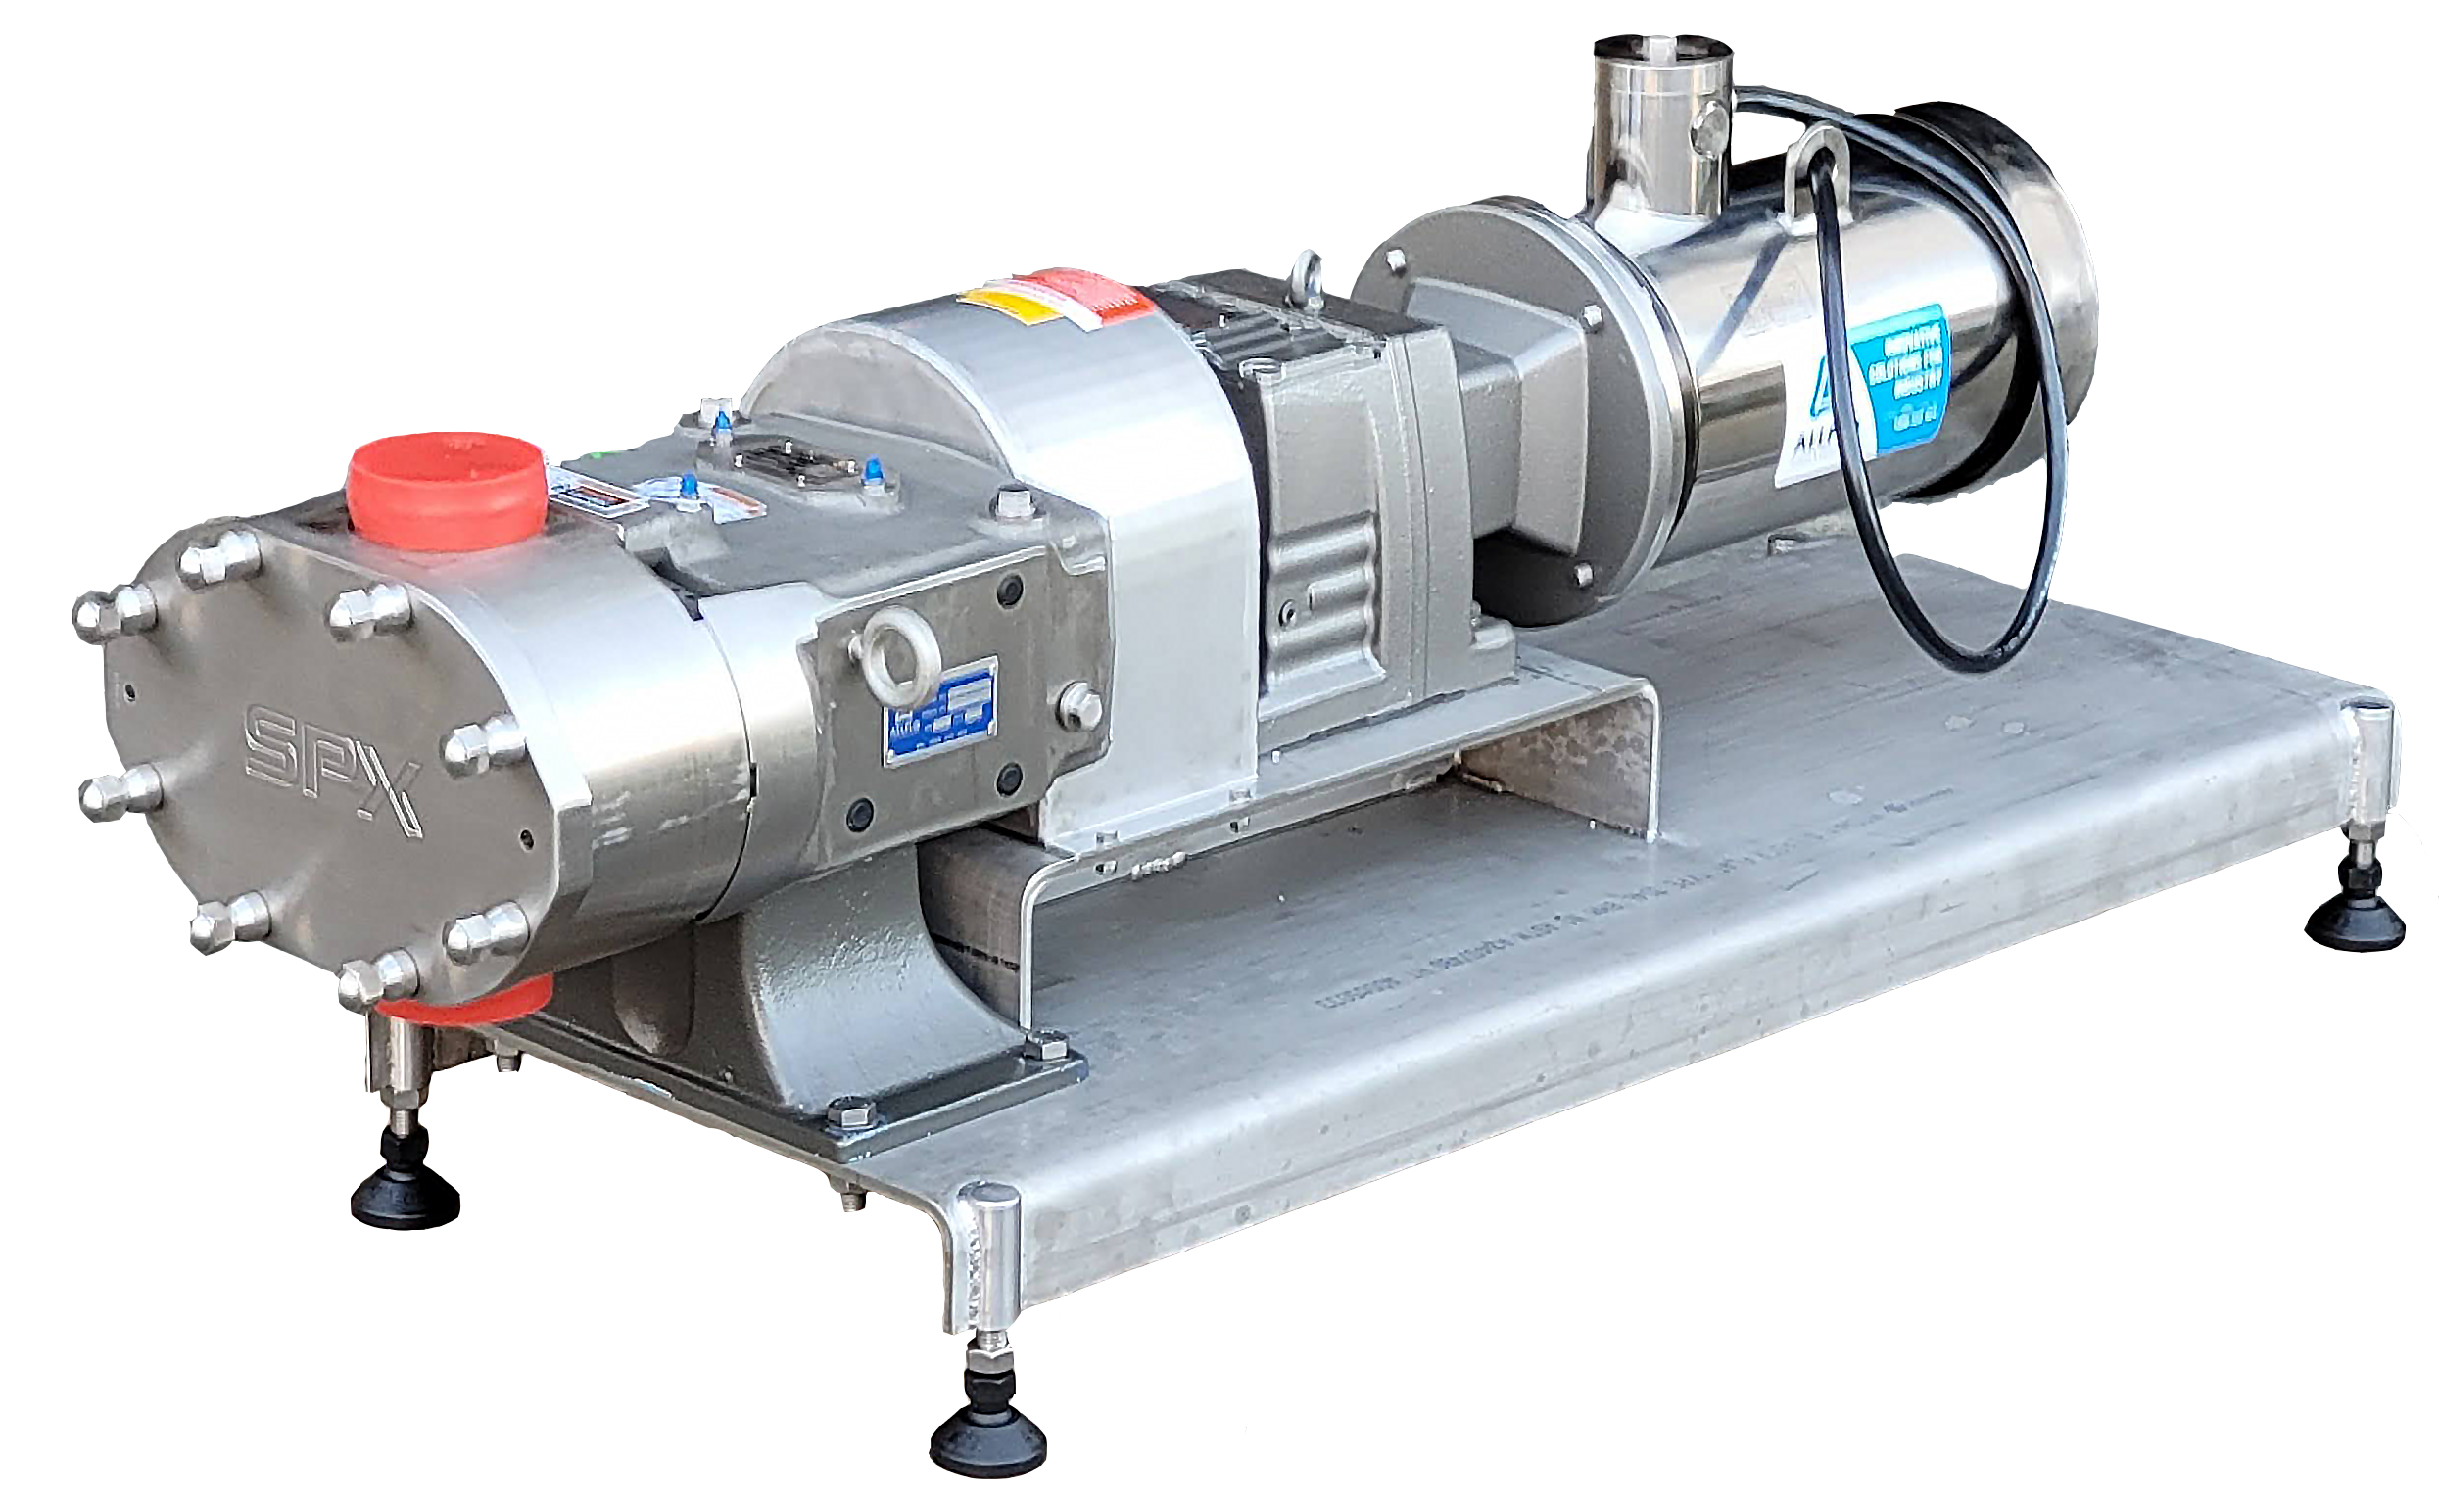
Custom pump base and Waukesha U3 pump solution designed to improve hygiene, maintenance safety, and efficiency in a high-volume dairy plant.
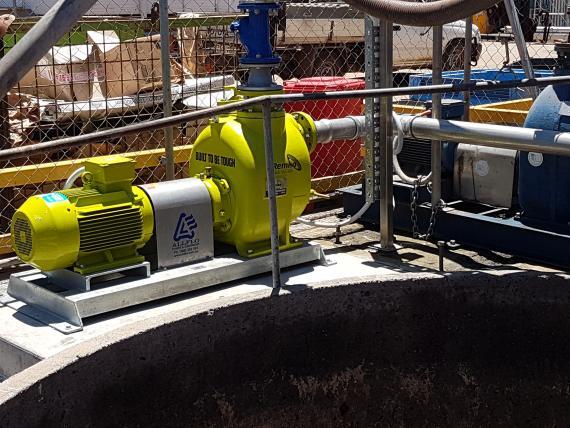
Heavy-duty Remko trash pumps selected for a Queensland abattoir trade waste upgrade, handling high solids and increased production demands.
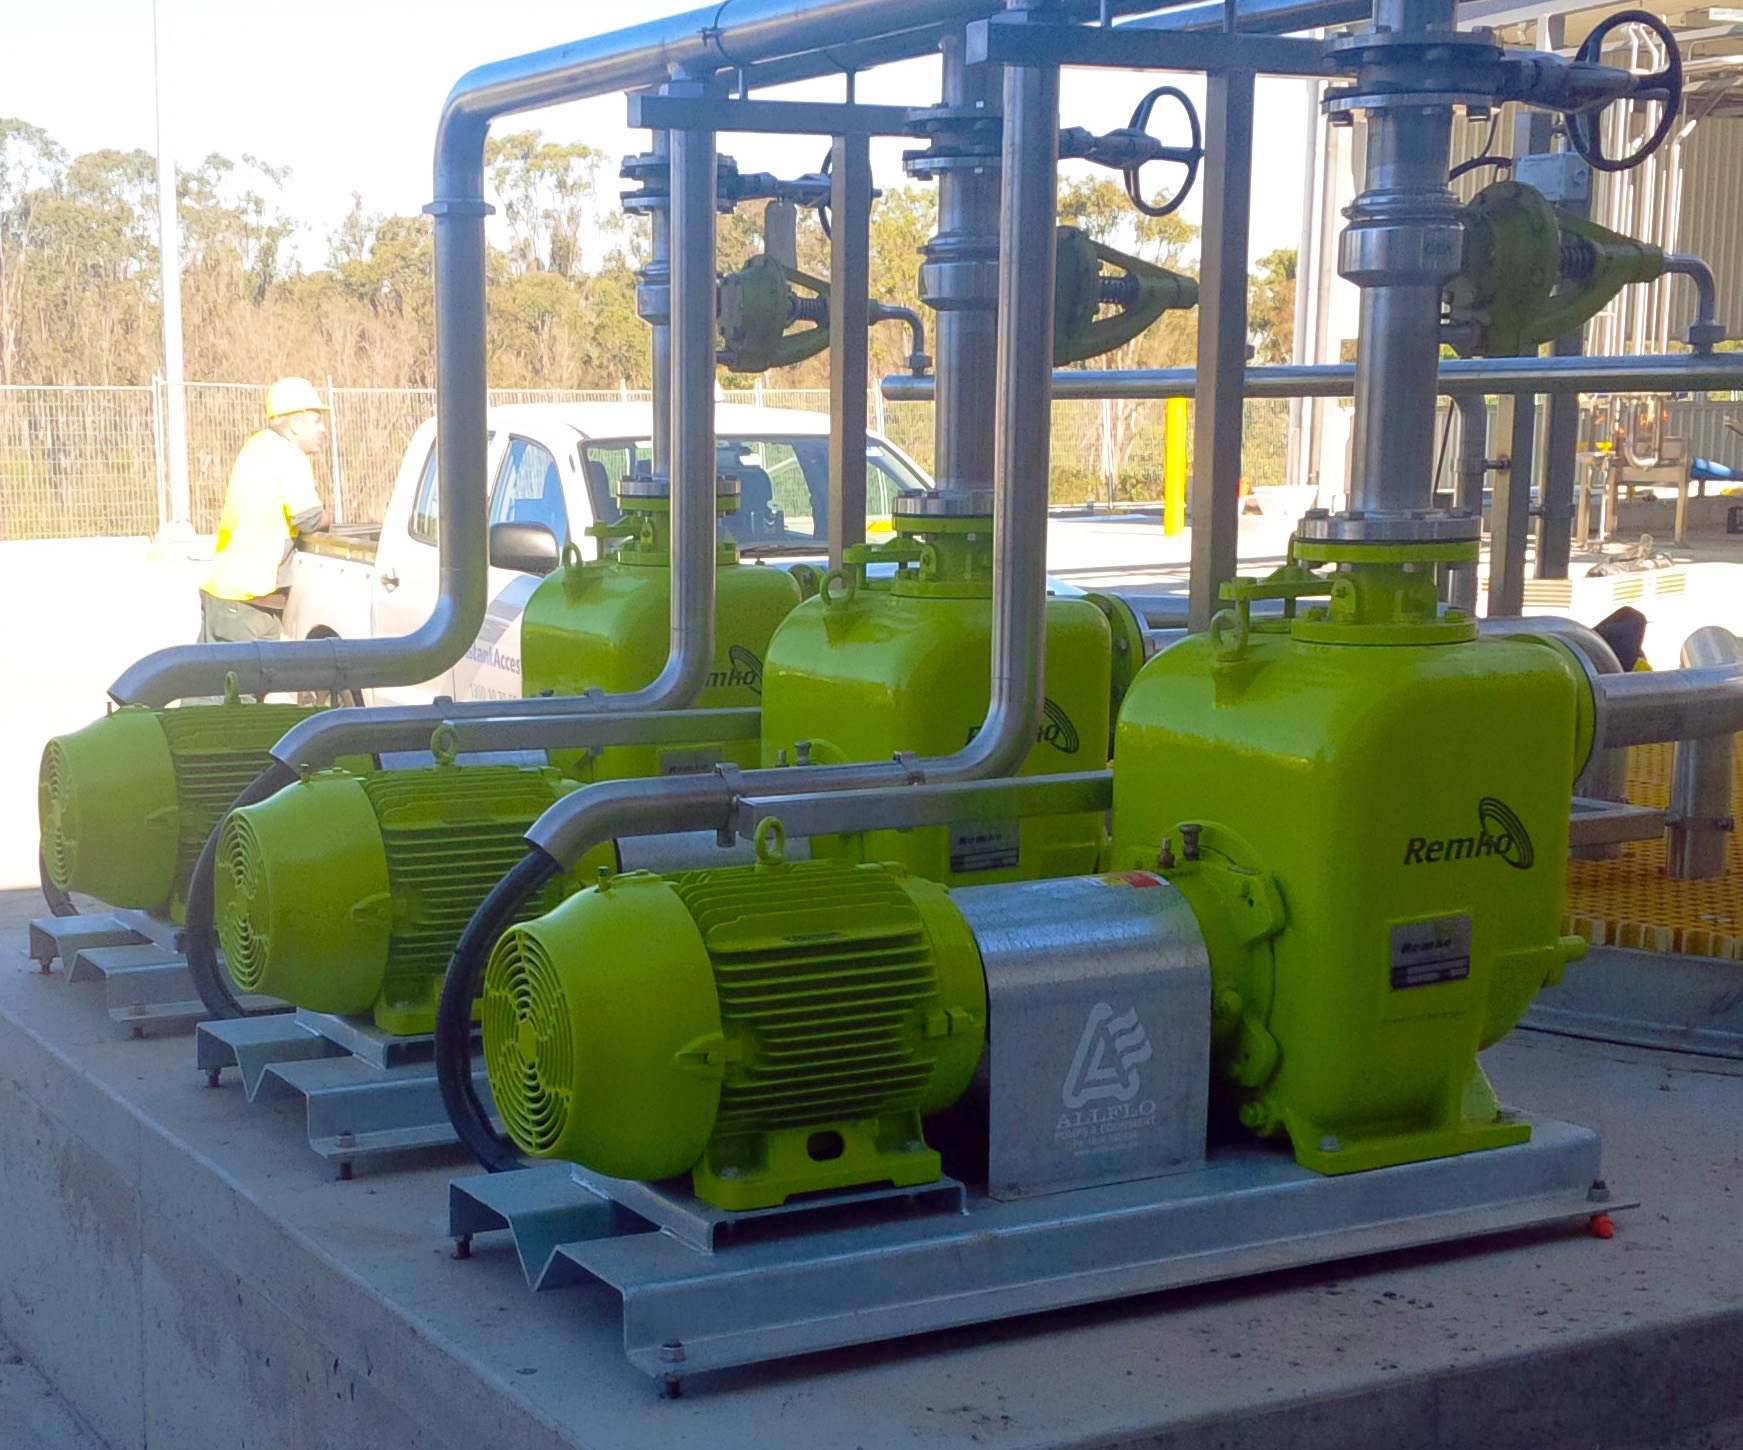
Engineered Remko trade waste pump systems supplied for Australian dairy manufacturing, designed for solids handling and long-term reliability.